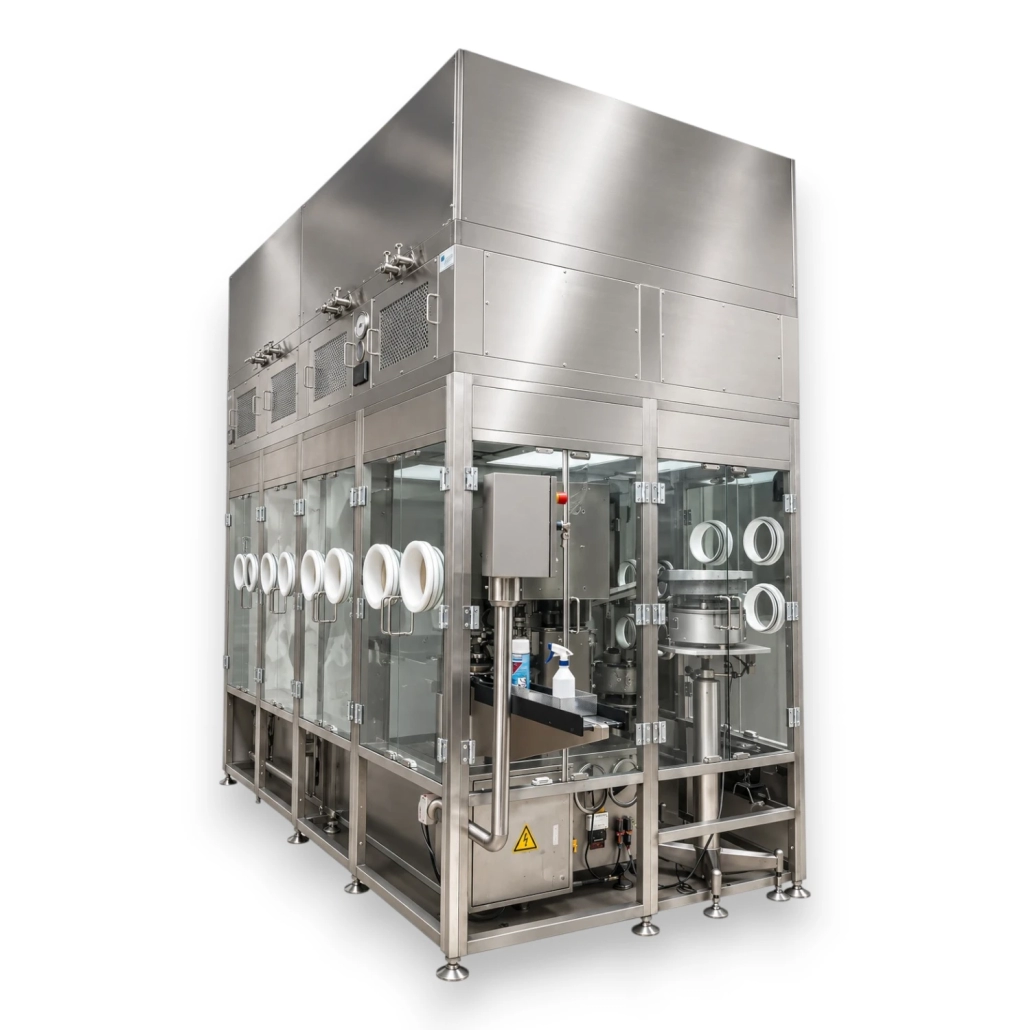
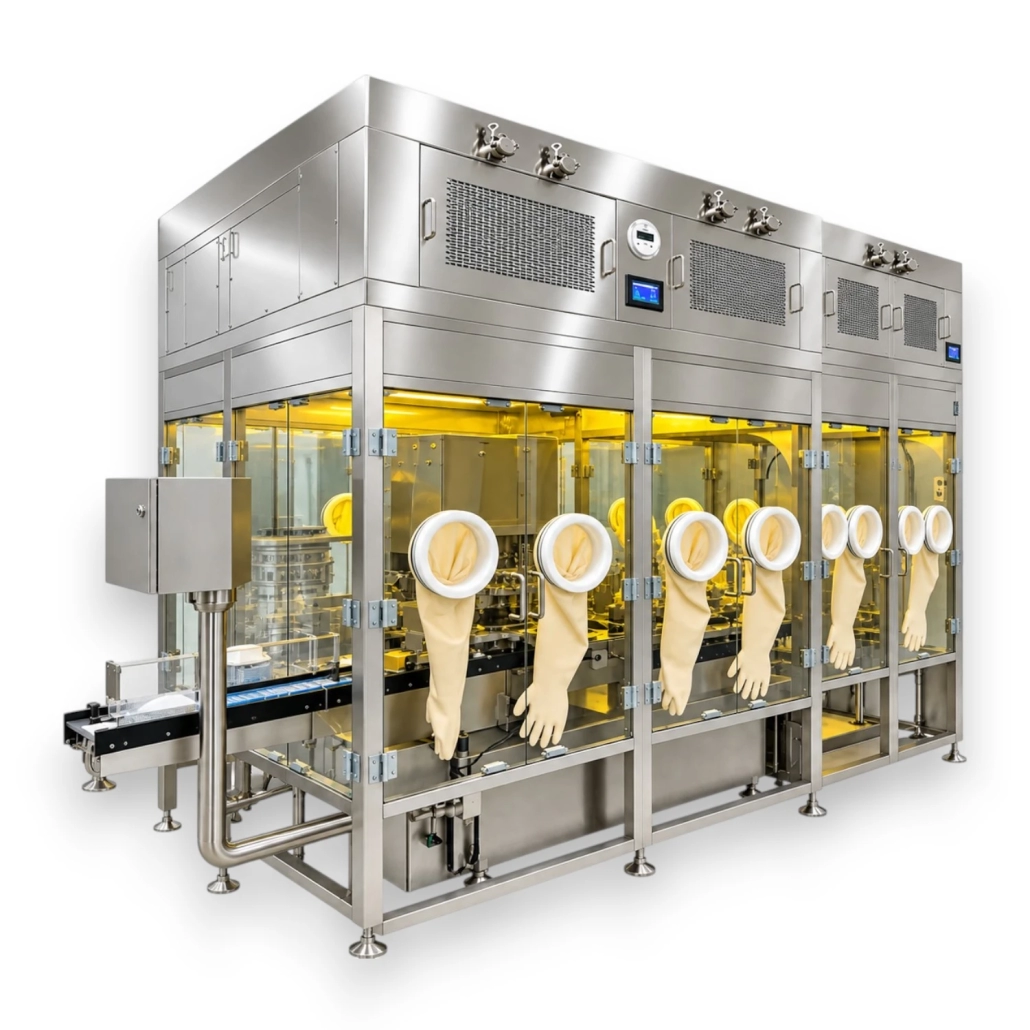
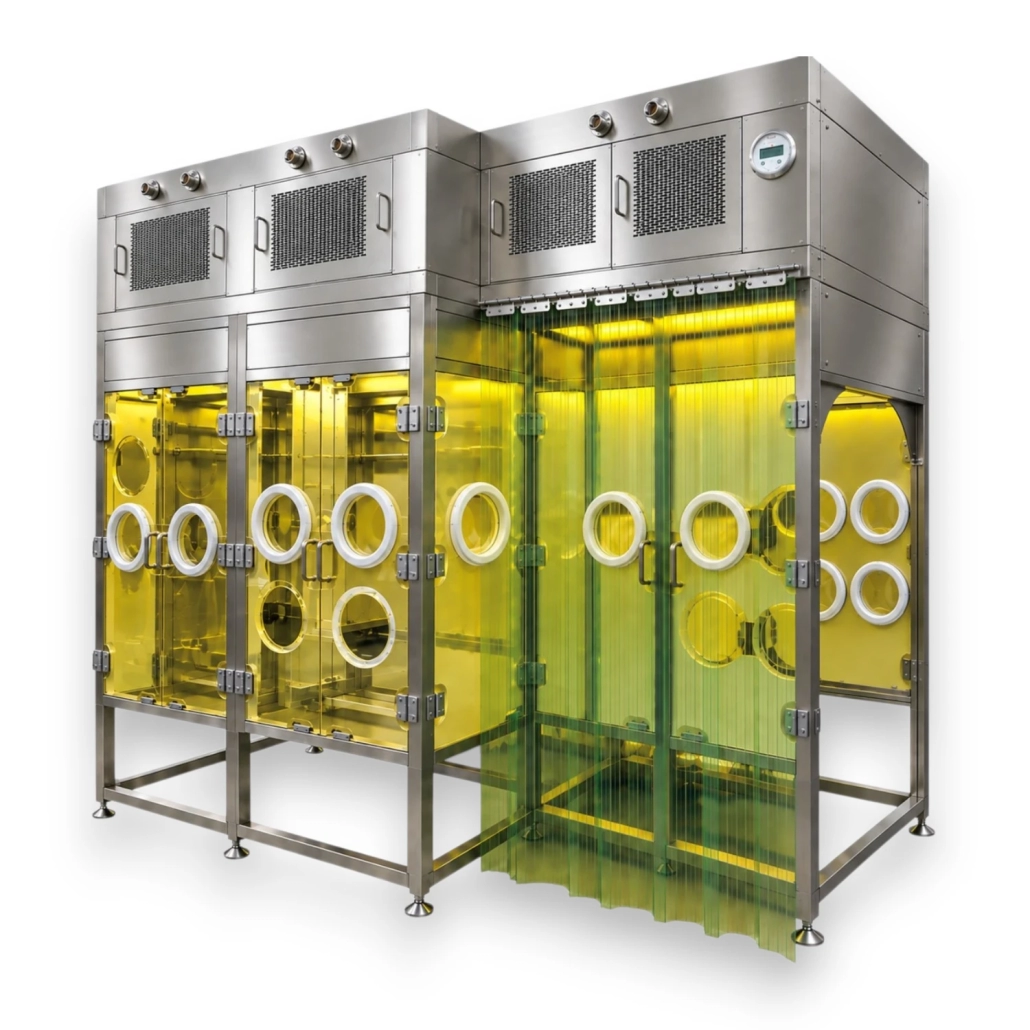
• Restricted Access Barrier System (RABS)

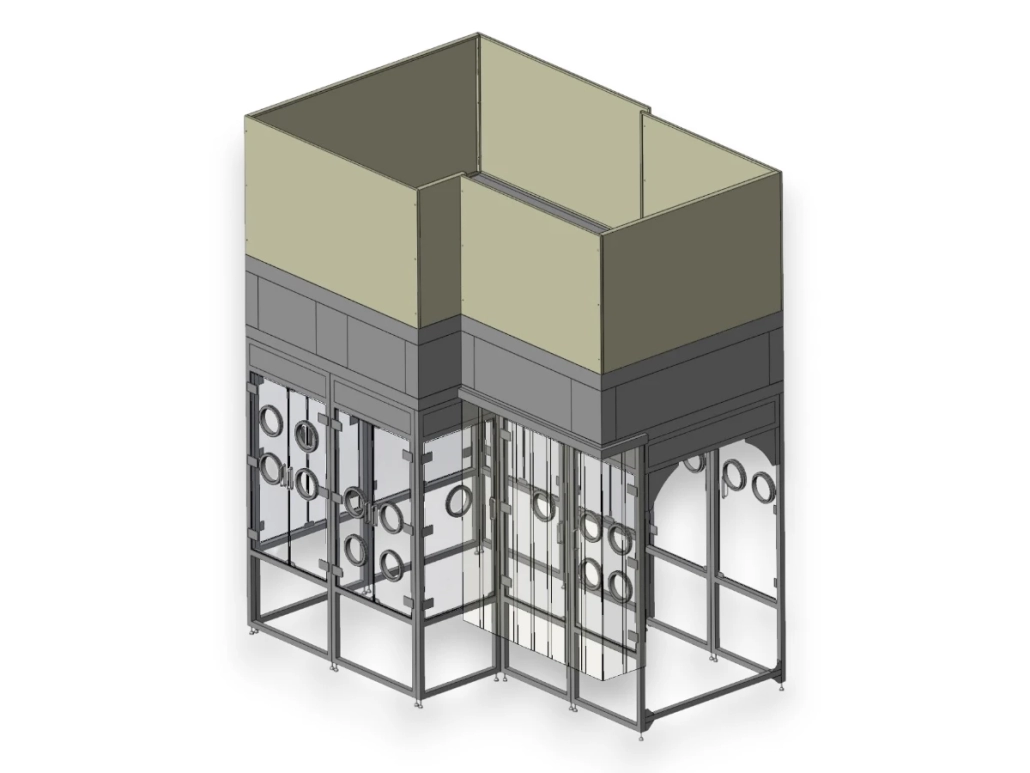
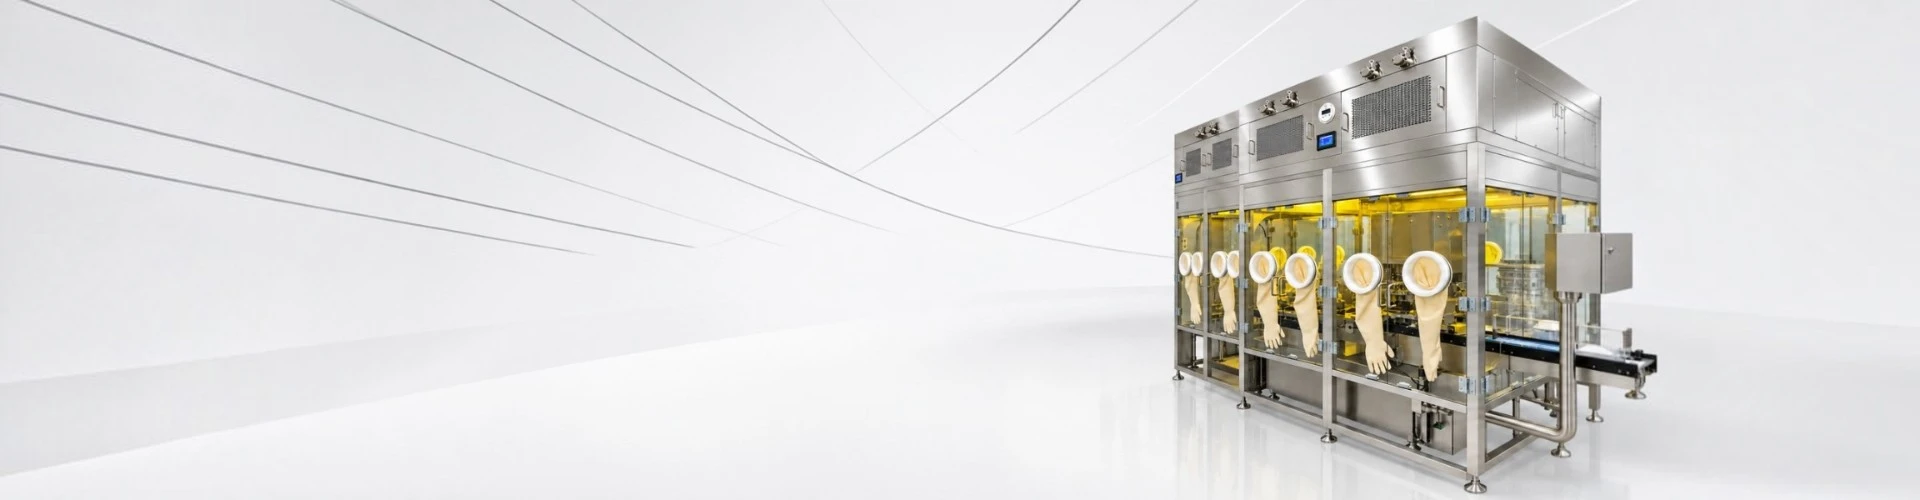
    Custom LAF+ RABS solutions for pharmaceutical and sterile manufacturing, providing ISO 5 protection around critical process equipment.
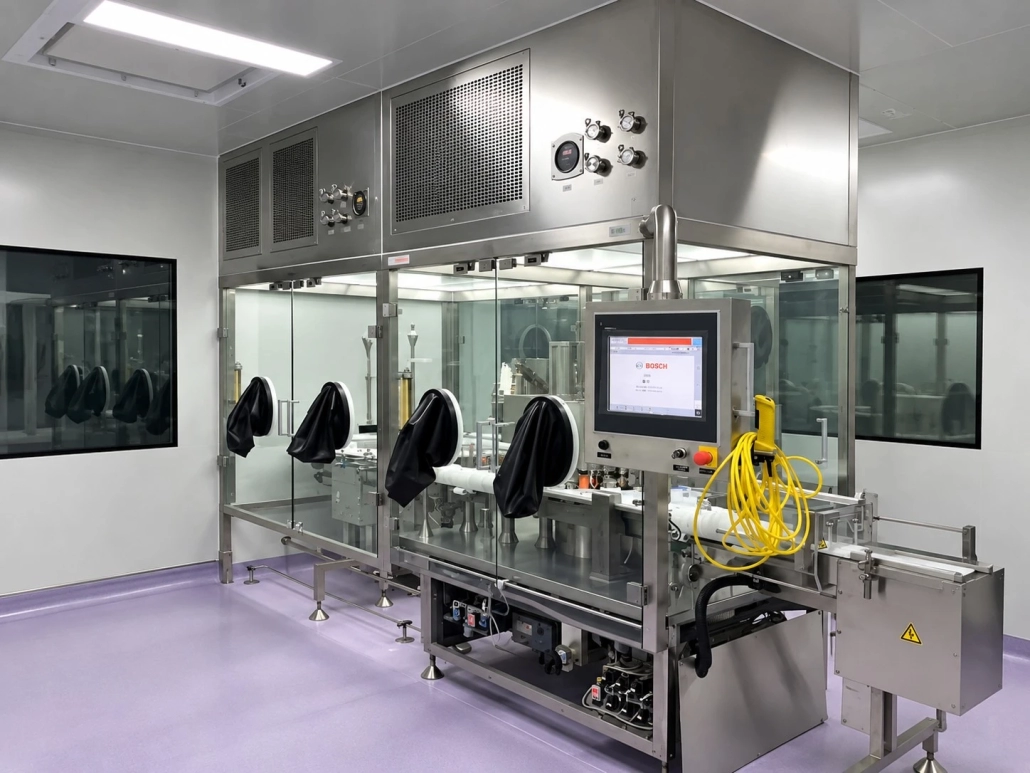
    Engineered for filling lines, processing equipment and cleanroom integration.

    Request a RABS Solution
    Restricted Access Barrier System

What is Restricted Access Barrier System?

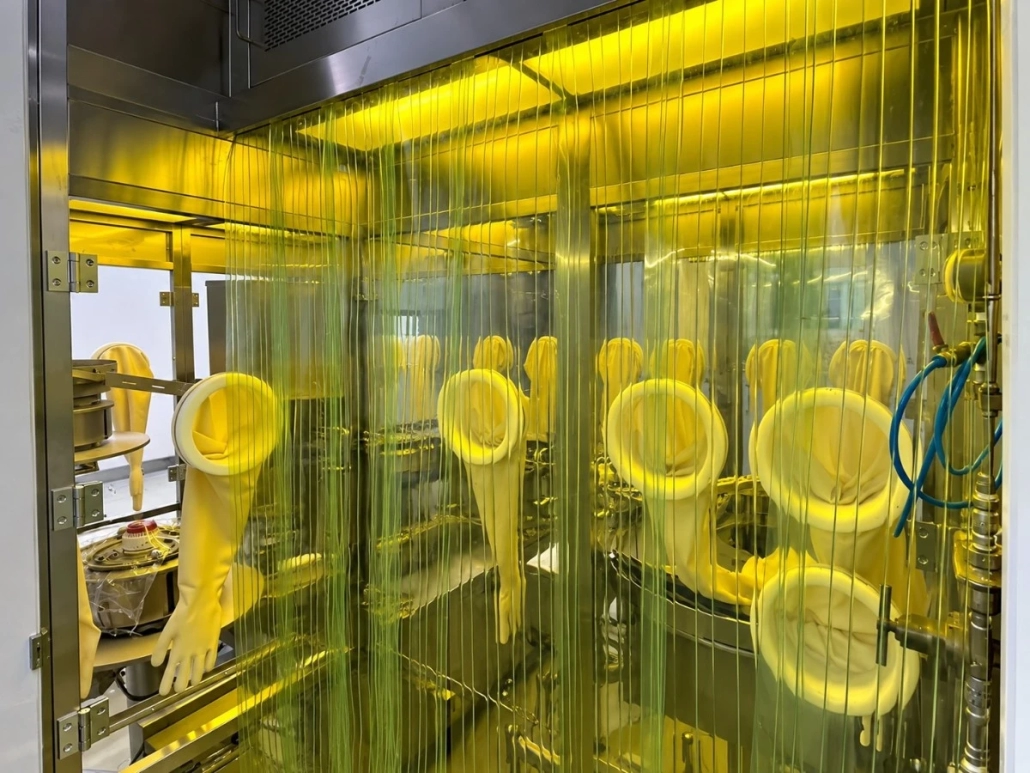
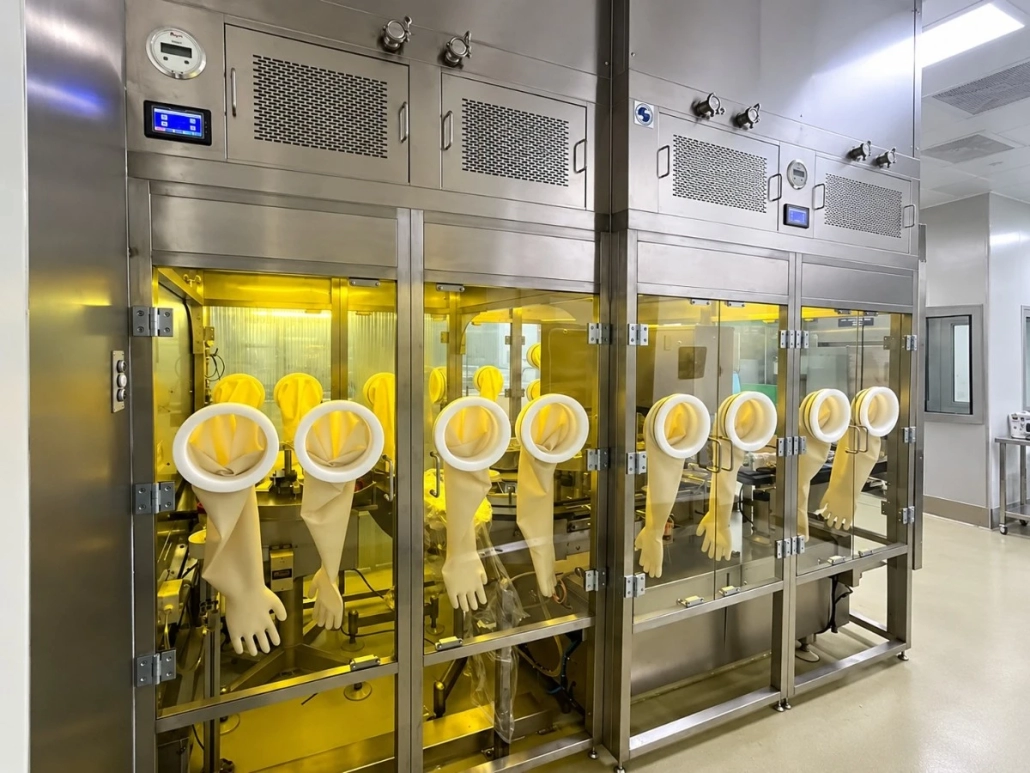
A Restricted Access Barrier System (RABS) creates a physical and aerodynamic barrier between operators and critical processing areas. HEPA-filtered unidirectional airflow, transparent barriers, controlled access and glove ports help maintain an ISO 5 critical zone while minimizing direct operator intervention.

Flair designs customized RABS around pharmaceutical process equipment, filling lines and cleanroom layouts.

  • Operator Protection: Physical physical barrier minimizes direct human intervention and particulate shedding.
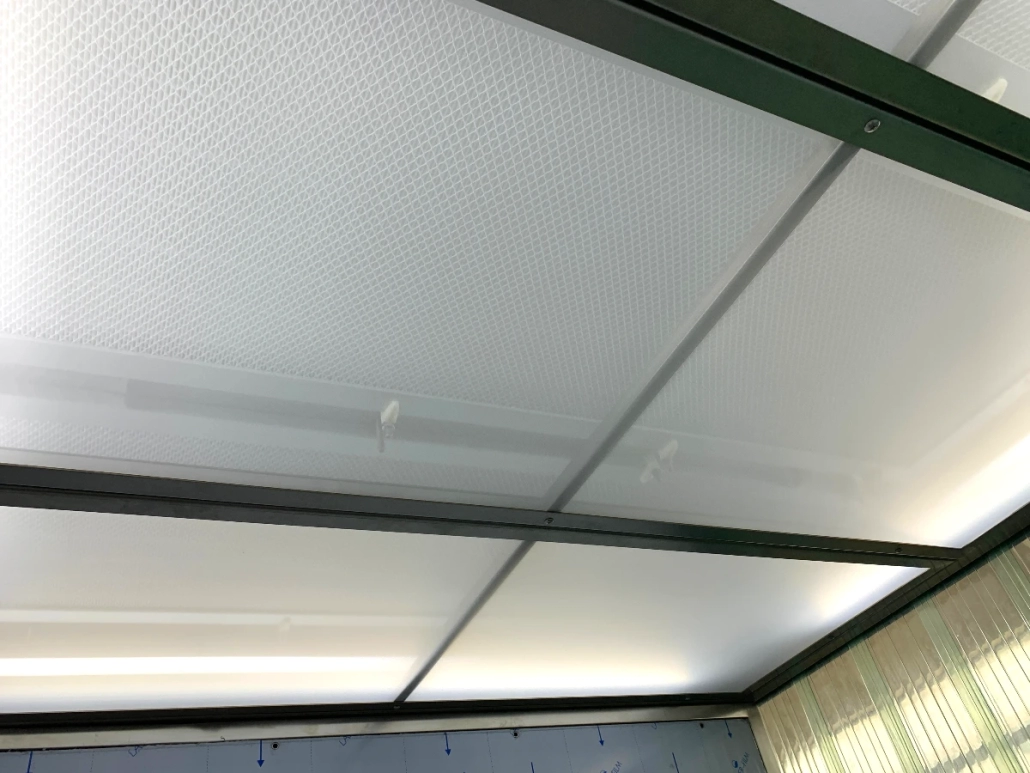
  • Product Protection: H14 GEL HEPA filtered unidirectional airflow sweeps away contaminants instantly.
  • Process Versatility: Seamlessly adaptable for passive RABS (pRABS) or active RABS (aRABS) configurations depending on your containment needs.
How Does a RABS System Work ?

Flair custom cleanroom equipment manufacturer

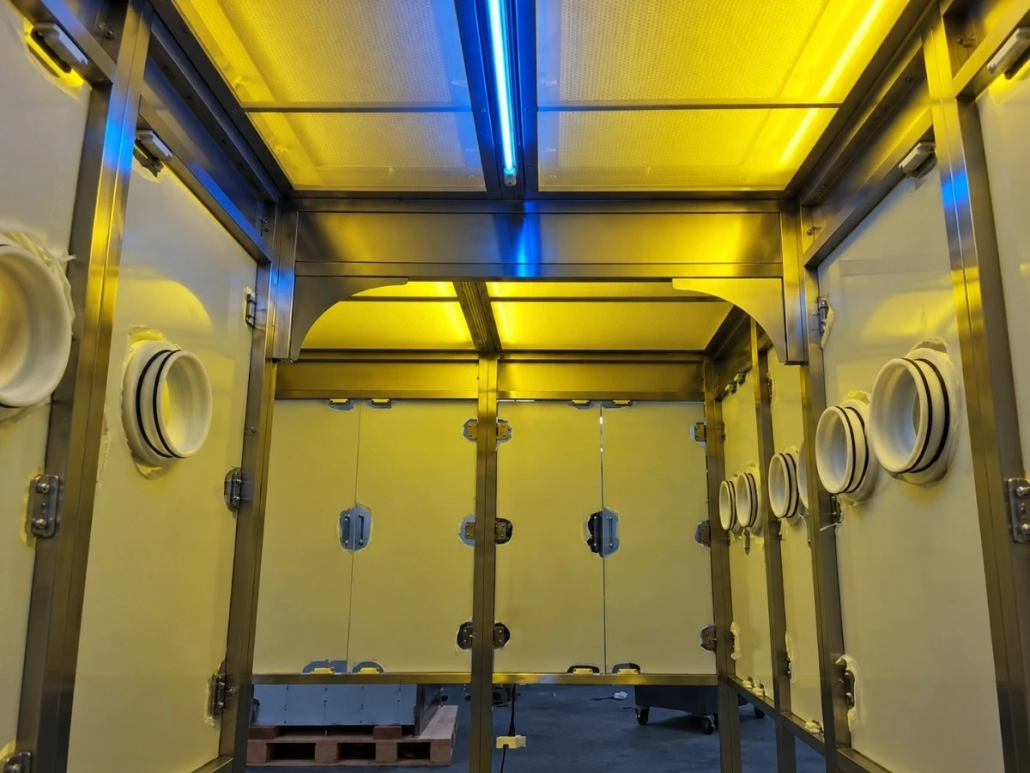
① HEPA-Filtered Air Supply

Filtered air is supplied to the protected process zone.

Flair custom cleanroom equipment manufacturer

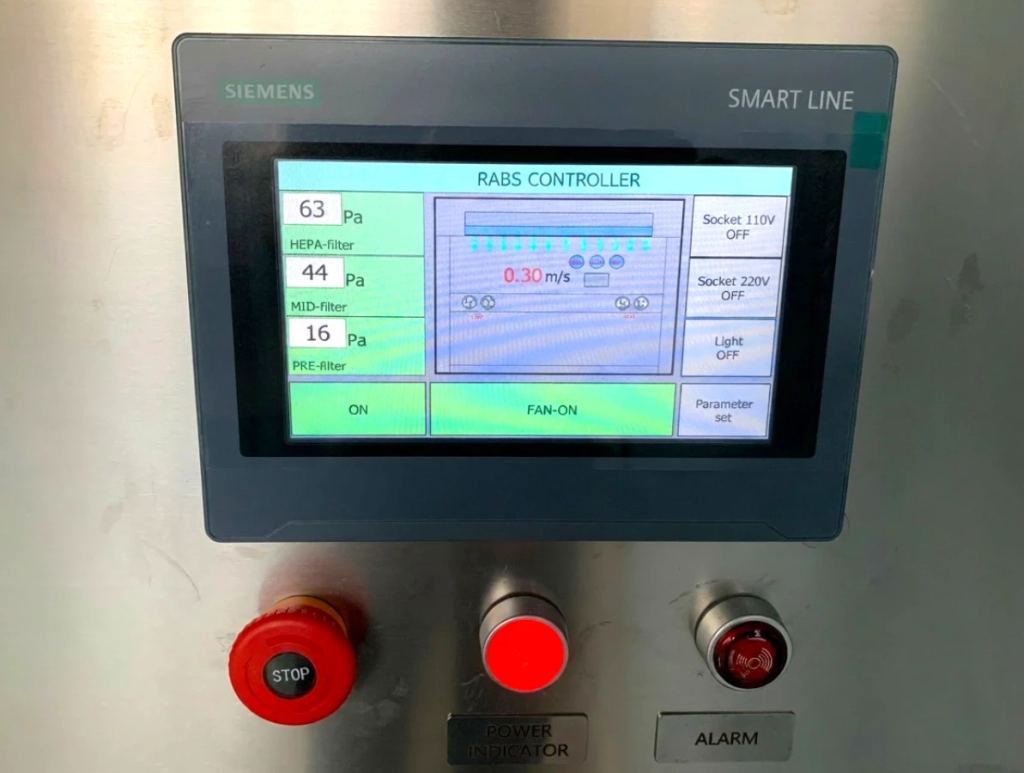
② HMI & Environmental Monitoring

Operating parameters and system status are monitored through the control interface.

Flair custom cleanroom equipment manufacturer

③ Physical Barrier Protection

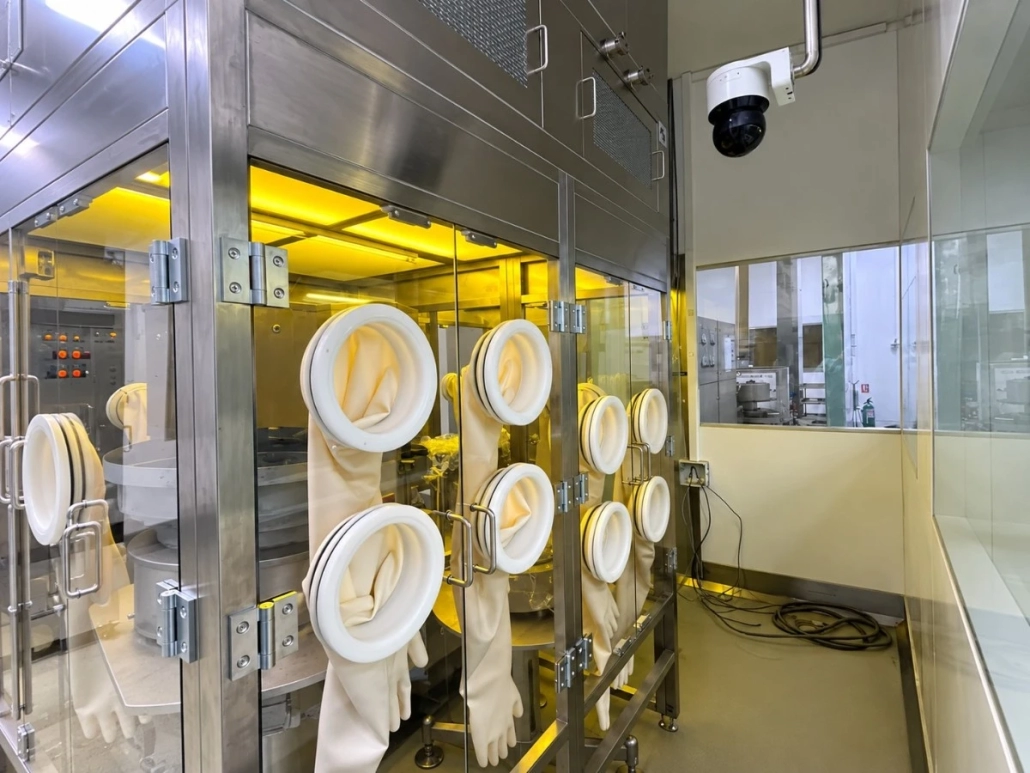
Transparent barriers and glove ports separate operators from critical processes.

Flair custom cleanroom equipment manufacturer

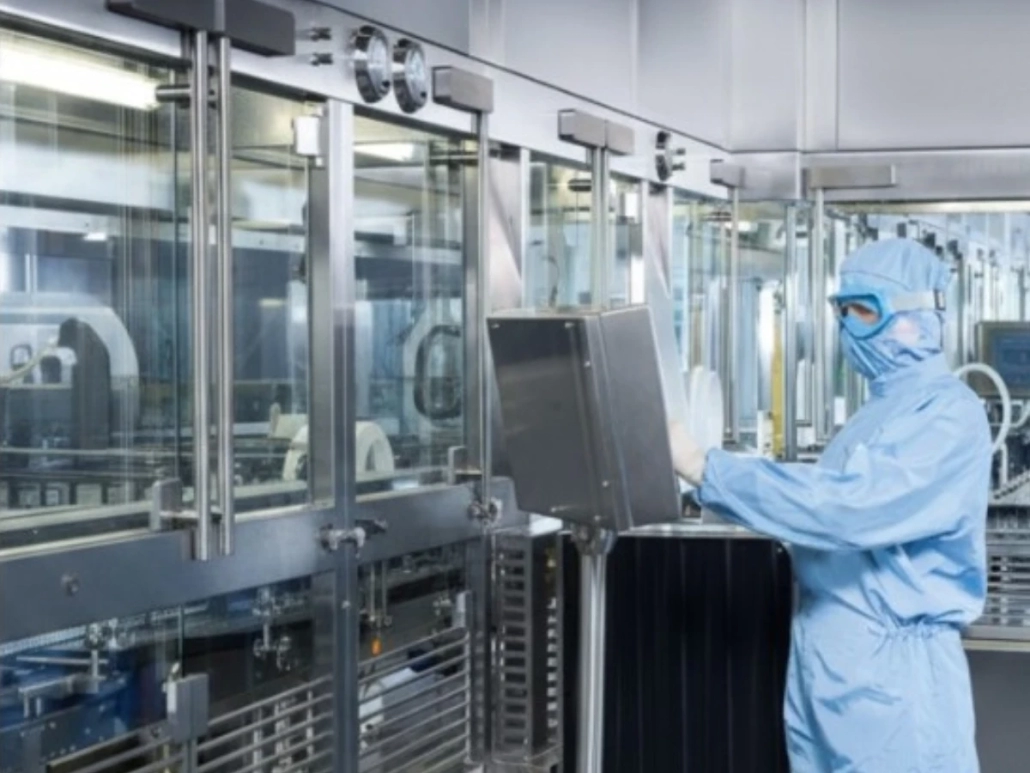
④ Controlled Operator Intervention

Glove ports and access doors allow controlled process intervention.

Main Components for Restricted Access Barrier Systems(RABS)

Flair custom cleanroom equipment manufacturer

Dual-Stage Air Filtration

H14 GEL HEPA filter+G4pre filter,At a uniform velocity (0.45 m/s+/-20%),Variable speed control

Flair custom cleanroom equipment manufacturer

Glove Port & Barrier Panel

Such as polycarbonate, tempered glass, or PETG featuring glazed sliding or hinged doors, integrated glove ports。

Flair custom cleanroom equipment manufacturer

HMI Control System

Touchscreen HMI,Provides intuitive operation and comprehensive monitoring

Flair custom cleanroom equipment manufacturer

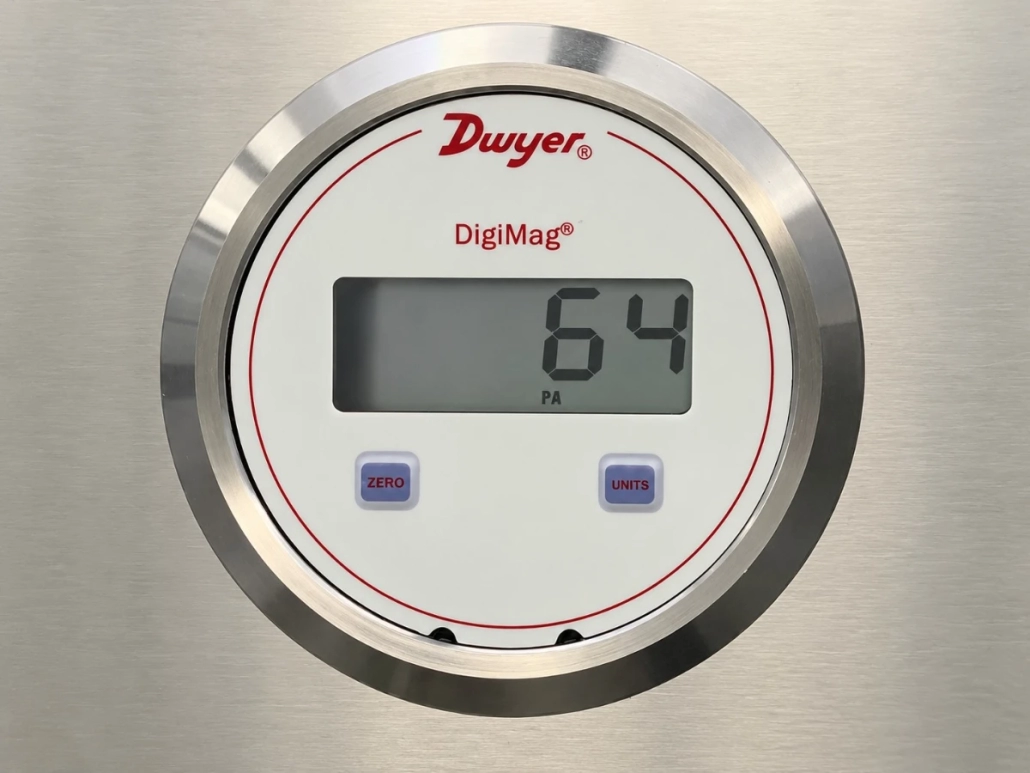
Dwyer Differential Pressure

Real-time pressure indication

Flair custom cleanroom equipment manufacturer

PAO/DOP Test Ports

DOP/PAO testing ports,Fully compatible with GMP validation.

Flair custom cleanroom equipment manufacturer

Compliance with International Standards

EU GMP Annex 1 &cGMP Guidelines,ISO 14644 Cleanrooms,EN1822 HEPA Filter Standard

Key Features of Restricted Access Barrier System

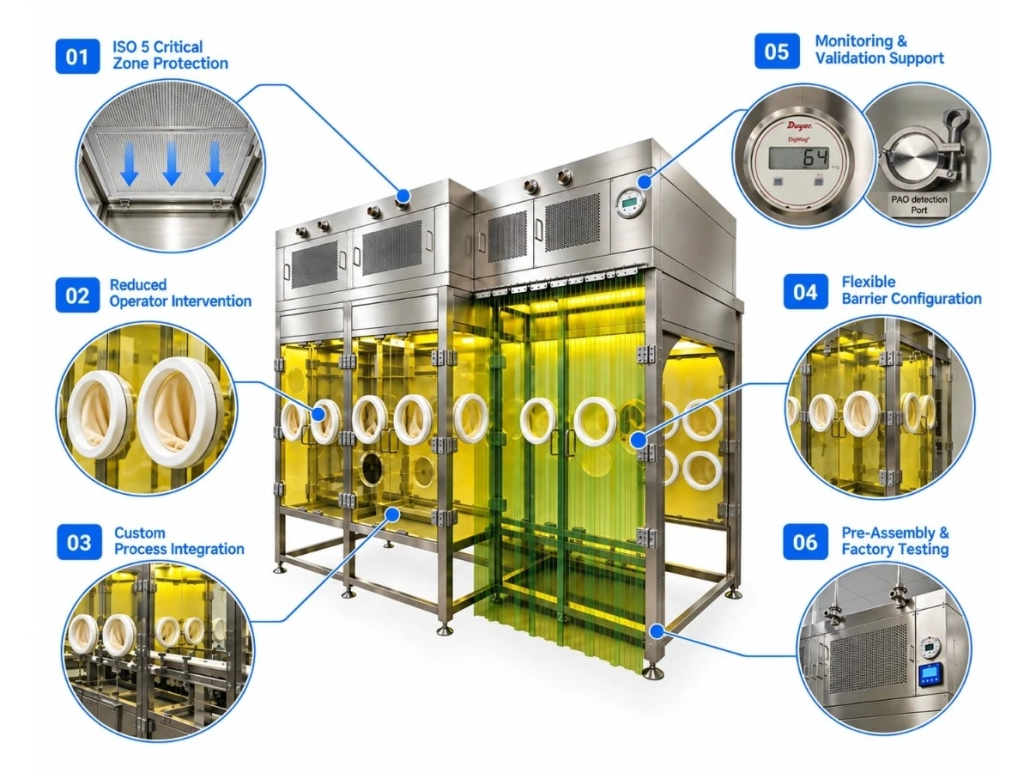
  • ① ISO 5 Critical Zone Protection

    Maintains HEPA-filtered unidirectional airflow over critical processes.

  • ② Reduced Operator Intervention

    Physical barriers and glove ports minimize direct contact with critical operations.

  • ③ Custom Process Integration

    Engineered around filling lines, process equipment and operating positions.

  • ④ Flexible Barrier Configuration

    Customized dimensions, doors, glove ports and access arrangements.

  • ⑤ Monitoring & Validation Support

    Designed with pressure monitoring and HEPA integrity testing provisions.

  • ⑥ Pre-Assembly & Factory Testing

    Pre-assembled and functionally tested before shipment to simplify site installation.

Restricted Access Barrier System features

Technical Specifications of RABS

Parameter

Standard Specification

Product Name Laminar Air Flow + Restricted Access Barrier System (LAF + RABS)
Cleanliness Classification ISO5 Class 100 (Grade A) Working Zone
Airflow Type Vertical Unidirectional (Laminar) Airflow
Average Air Velocity 0.45 m/s ±20% (Adjustable: 0.30–0.70 m/s)
Filtration System Dual-stage Filtration (G4 Pre-filter + H14 GEL HEPA Filter)
Construction SUS304 / SUS316L
Barrier Tempered glass / transparent panel
Glove Ports Customized quantity & position
Differential Pressure Monitoring Dwyer Differential Pressure Gauge (Standard)
Control Touchscreen HMI (Standard)
Lighting LED Cleanroom Lighting/Yellow lighting option
Dimensions Customized
Installation Type Floor-mounted / Integrated Production Line
Qualification Support FAT, SAT, IQ, OQ, PQ Documentation Available

Detailed specifications are engineered according to process equipment, URS and cleanroom requirements.

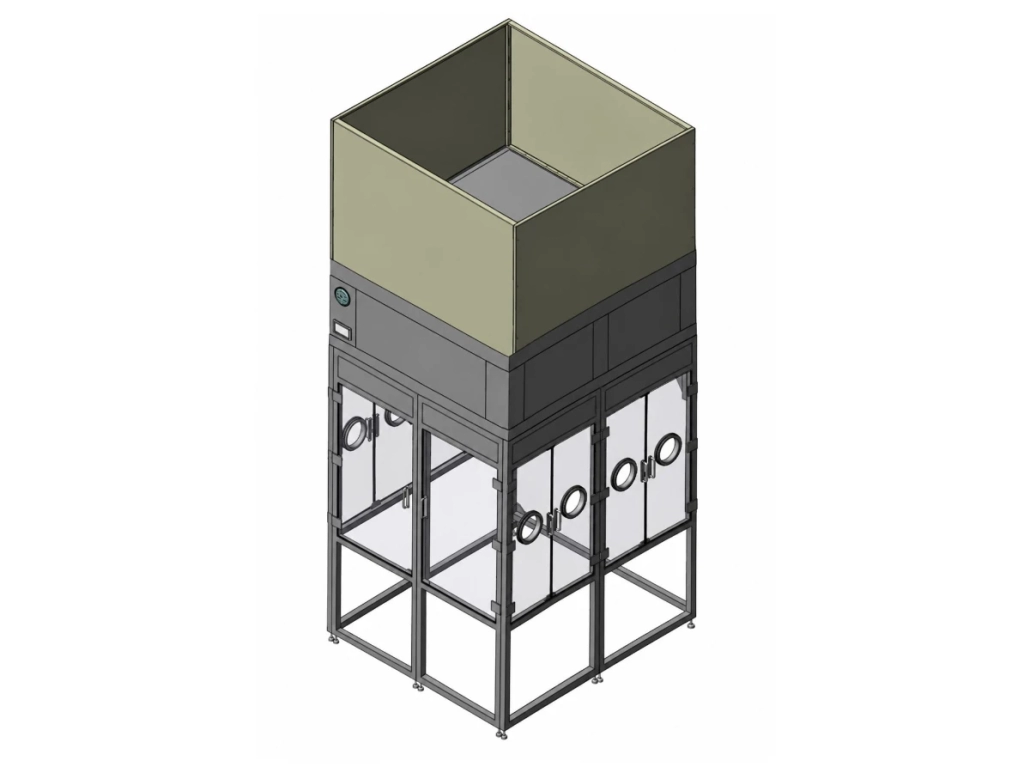
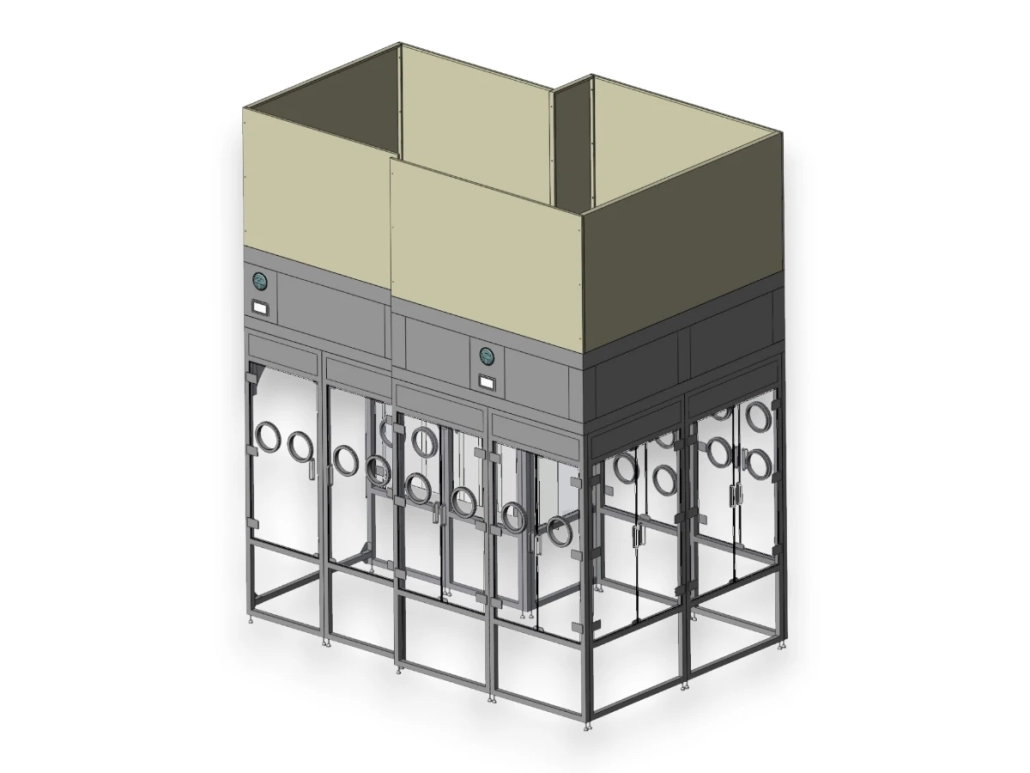
Custom RABS Engineering and Process Integration

Every RABS project is engineered around the process—not selected from a fixed standard size. Flair coordinates the barrier layout, airflow system, glove-port positions, equipment interfaces and cleanroom integration according to the customer’s URS and process requirements.

  • Process equipment dimensions
  • Glove-port positioning
  • Barrier configuration
  • Airflow & HEPA layout
  • Utility/interface coordination
  • FAT & site installation requirements

From URS to Installation

Requirements / URS

01

RABS Engineering Design

02

Manufacturing / FAT

03

Delivery / Site Installation

04

Testing / Validation Support

05

Project References

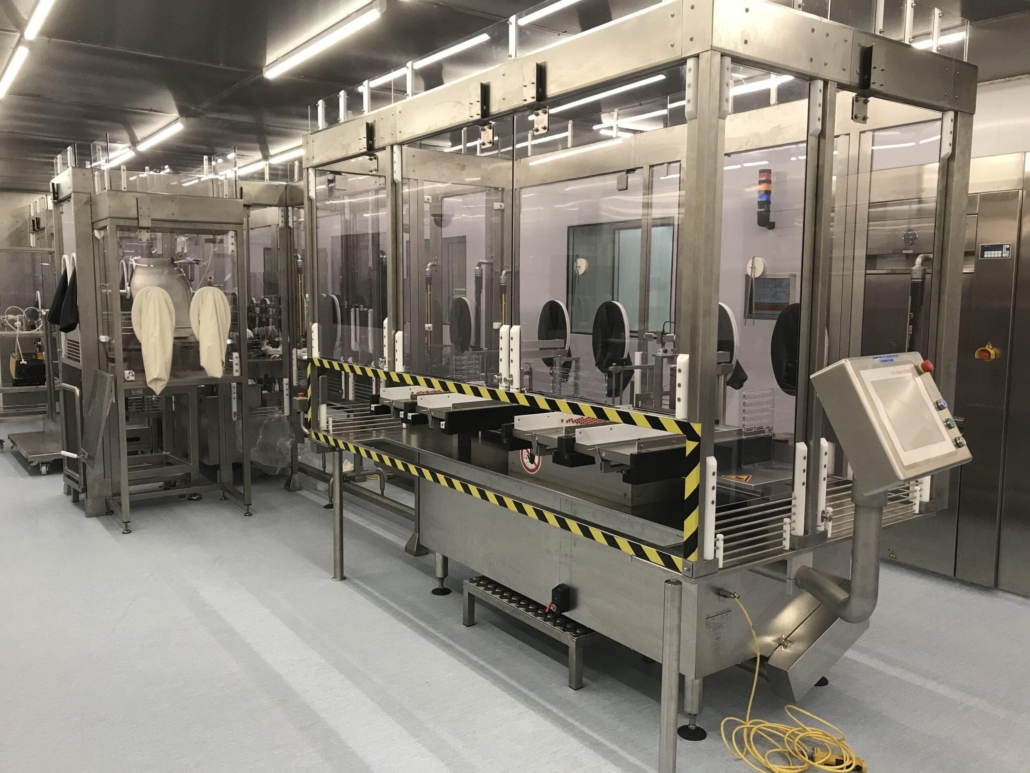
customized LAF + RABS system for aseptic pharmaceutical manufacturing

Pharmaceutical Processing RABS

  • Project Snapshot
    Customized multi-station RABS designed around pharmaceutical processing equipment to provide controlled protection for critical operations.
  • Project Requirement
    The barrier layout needed to accommodate existing equipment, multiple operator positions and restricted-access requirements within the available cleanroom space.
  • Flair Solution
    Custom glove-port positioning, H14 HEPA-filtered airflow, transparent barrier panels and integrated monitoring were configured around the process layout.
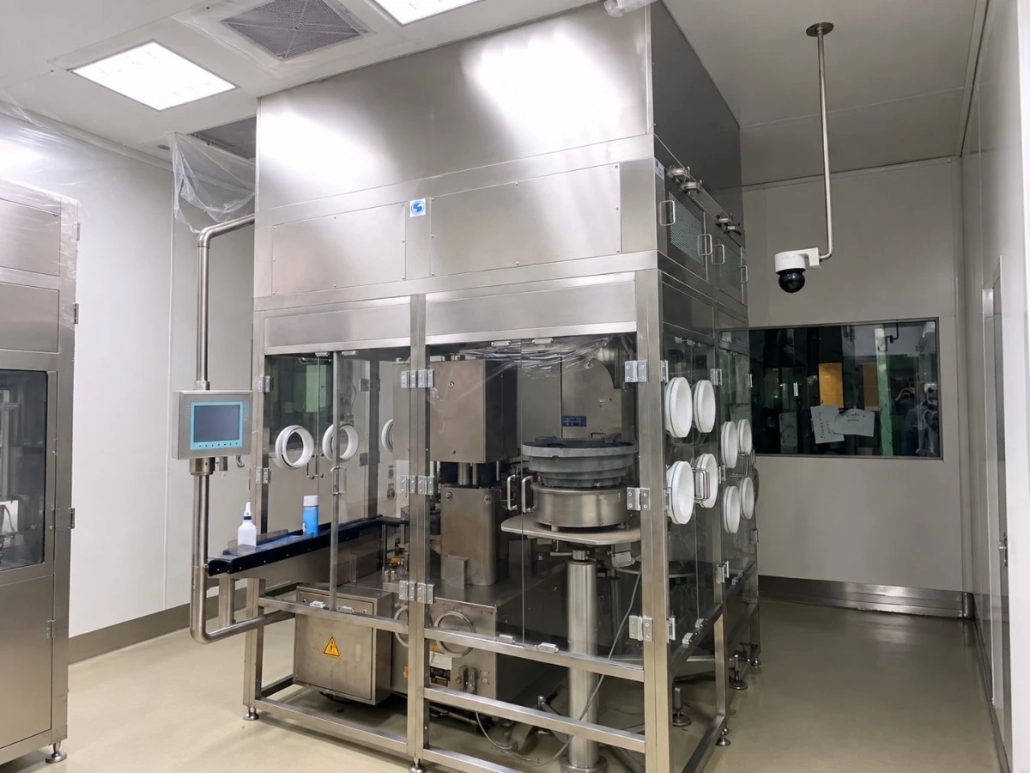
customized LAF + RABS system for aseptic pharmaceutical manufacturing

Customized RABS for Controlled Processing

  • Project Snapshot
    Custom RABS integrated around existing production equipment for contamination-sensitive pharmaceutical processing.
  • Project Requirement
    Multiple operating positions required convenient glove access while maintaining physical separation between operators and the controlled process zone.
  • Flair Solution
    The system was engineered with customized glove-port locations, HEPA-filtered airflow, transparent access panels and HMI-based monitoring to suit the equipment arrangement.
ISO Class 5 Restricted Access Barrier System

RABS for Aseptic Filling Line

  • Project Snapshot
    RABS integrated with pharmaceutical filling equipment to protect critical filling and handling operations.
  • Project Requirement
    The filling process required controlled operator access while maintaining a protected environment around critical product-exposure areas.
  • Flair Solution
    The RABS combines HEPA-filtered airflow, glove-port access, transparent barriers and process monitoring while allowing integration with the filling equipment and cleanroom layout.

RABS vs Laminar Flow Hood vs Isolator

RABS, laminar flow hoods and isolators provide different levels of process separation and contamination control. The appropriate solution depends on process risk, operator access and containment requirements.

Feature

Laminar Flow Hood (LAF)

RABS (Restricted Access Barrier System)

Isolator

Physical Barrier None (Open-front configuration) Rigid glass/polycarbonate walls with glove ports Completely sealed, pressure-tight enclosure
Operator Access Unrestricted access to the work zone Restricted access via integrated glove ports & sliding doors Strictly restricted via glove ports or half-suits
Cleanliness Standard ISO Class 5 / EU GMP Grade A (local zone) ISO Class 5 / EU GMP Grade A ISO Class 5 / EU GMP Grade A
Sterilization Method Manual surface wipe-down (IPA / Sporicides) Manual wipe-down or semi-automated cleaning Automated gaseous bio-decontamination (VHP)
Airflow Dynamic Unidirectional vertical or horizontal laminar flow Unidirectional laminar downflow with return paths Recirculated or exhausted laminar flow through tight seals
Capital Investment Low Moderate to High Premium (Very High)
Operator Ergonomics Maximum freedom of movement High ergonomic flexibility and intervention capability Moderate (restricted entirely by glove reach)

RABS industrial applications&solutions

RABS solutions are widely used to protect critical pharmaceutical processes where ISO 5 airflow, physical separation and controlled operator access are required.

Controlled Access for RABS System

Aseptic Filling & Closing

RABS protection for critical filling, stoppering and closing processes.

ustomized LAF + RABS system for aseptic pharmaceutical manufacturing

Sterile Pharmaceutical Processing

Controlled barrier protection around contamination-sensitive pharmaceutical equipment and operations.

Pharmaceutical Manufacturing with RABS

Equipment & Process Integration

Customized RABS integrated around critical process equipment and production layouts.

FAQs

Find answers to frequently asked questions about our products. See the most common topics and more. Any other questions just feel free to contact us.

Full name is Restricted Access Barrier System.

A RABS is a cleanroom containment enclosure combining rigid physical barriers and laminar airflow to isolate sensitive sterile processes from human operators.

RABS provides barrier separation inside cleanrooms, while isolators offer a more complete enclosed isolation environment.

A RABS typically maintains ISO Class 5 (ISO 14644-1) or EU GMP Grade A conditions in the critical work zone.

Yes, dimensions, airflow, glove ports and control systems can be customized.

The nominal downward airflow velocity is maintained at $0.45 m/s+/-20%

Terminal H14 GEL HEPA filters are generally replaced every 12 to 24 months based on differential pressure drop and annual integrity test results.G4 pre filter should be replaced per 3-6 months;

Yes, our systems are engineered to meet or exceed EU GMP Annex 1 requirements regarding human intervention reduction and Grade A containment.

Pharmaceutical manufacturing, biotechnology, sterile compounding pharmacies, vaccine production, and advanced medical device assembly.

Yes, custom RABS units are specifically engineered to house and enclose automated vial, syringe, and liquid filling machinery.

Yes, comprehensive FAT protocols and documentation are executed at our manufacturing plant prior to crating and export.

Depending on frequency of use and sterilization cycles, EPDM or Hypalon gloves typically require routine inspection and periodic replacement.

Yes, glove port height, spacing, and port ring dimensions are customized based on ergonomic studies and client preference.

Yes, modular RABS units are designed for straightforward assembly and integration into pre-existing cleanroom.

Need a Custom RABS Solution? Request a Quote

Copyright © 2018 - 2026 Shenzhen Flair Equipment Co., Ltd.